
How to Prevent Score Cracking in Folding Cartons: A B2B Production Guide
Folding carton score cracking is not one defect with one universal fix. A visible white line may be exposed paper fibres, an ink break, a coating crack, laminate whitening or another surface-layer symptom. The practical goal is to reduce risk by reviewing the board, grain direction, crease system, artwork, surface finishes, folding conditions, samples and acceptance standard as one job-specific system.
Quick Answer
To reduce score-cracking risk, identify the visible symptom first, then review the paperboard, grain direction, board condition, crease rule and matrix, print coverage, coating or lamination, special finishes, fold direction and sample result together. Do not apply one crease setting or one grain rule to every carton. Mark fold-sensitive artwork on the dieline, approve a production-relevant sample when appearance is critical and agree on the visual acceptance standard before mass production.
Key Facts for Packaging Buyers
- Creasing prepares paperboard to fold; the board and tooling need to be matched for the job.
- Fibre cracking, ink cracking, coating cracking and laminate whitening are different symptoms.
- Grain direction affects stiffness and folding behavior, but there is no universal orientation rule for every carton.
- Board type, thickness, coating, storage condition and moisture history can change fold behavior.
- Dark solid colors can make white fibres and surface cracks more visible.
- Lamination, foil, embossing and Spot UV near a fold should be reviewed before the artwork is finalized.
- A digital proof does not reproduce the final crease and fold system.
- Samples reduce uncertainty but do not create a defect-free production guarantee.
- Buyers should define the visual acceptance standard before mass production.
What Score Cracking Looks Like
Before discussing a cause, describe what is actually visible. Buyers often use “cracking” for several different effects. A fold can expose broken fibres in the paperboard. Ink can split while the fibres remain largely intact. A coating can form fine surface lines. A laminate can turn white under stress or begin to separate. These symptoms can appear together, but they are not automatically the same failure.
| Visible symptom | Possible layer involved | What to review |
|---|---|---|
| White fibres exposed at the fold | Paperboard fibre structure | Board, grain, crease geometry, folding direction and board condition. |
| Printed color breaks but fibres are less visible | Ink or printed surface | Ink coverage, drying, coating, board surface and fold strain. |
| Fine surface lines in a coated area | Paper coating or applied coating | Coating stack, crease, board, fold and sample result. |
| Milky or white line in a laminated area | Film or adhesive interface | Film, adhesive, board, crease, fold direction and temperature history. |
| Surface layer begins to lift or separate | Coating, laminate or board layer | Material compatibility, conversion, storage and folding conditions. |
A close-up photo helps describe the symptom, but it does not prove the root cause. Send the supplier the finished carton, flat blank, dieline, board description and finishing specification whenever possible.
Why Paper Grain Direction Matters
Paperboard fibres have a machine direction and a cross direction. This directional structure changes stiffness, bending and fold response. Grain direction is therefore an important review factor, especially when a carton has long folds, narrow panels, reverse folds or a premium surface where a small white line is unacceptable.
However, “always run the grain parallel to the fold” or “always run it perpendicular” is too simple for real production. The preferred orientation can depend on the board construction, carton shape, panel dimensions, fold sequence, stiffness requirement and die layout. Changing grain direction may improve one fold while affecting another panel or the sheet yield.
Buyers do not need to prescribe the grain direction themselves. They should provide the structural dieline and visual priorities, then ask the paperboard and packaging supplier to review grain as part of the complete job.
Buyer question to add to the technical brief
“Has grain direction been reviewed against the critical folds, carton stiffness and sheet layout for this board and structure?”
Board Type, Thickness and Moisture Condition
Different paperboards have different fibre structures, layers, coatings and bending behavior. Solid bleached, folding boxboard, recycled-content board, kraft board and other constructions should not be expected to use the same crease setup or show the same fold appearance. Even two boards with a similar nominal thickness can behave differently.
Board condition also matters. Storage, transport and seasonal humidity can change the way paperboard bends and how the surface responds. The correct response is not to publish one universal moisture percentage. It is to keep the material identified, stored consistently and reviewed under production-relevant conditions.
| Factor | Why it matters | Buyer action |
|---|---|---|
| Board construction | Fibre layers, coating and density affect fold behavior. | Approve the exact board direction rather than only a generic GSM. |
| Thickness and stiffness | Thicker or stiffer boards change crease and folding requirements. | Provide the product weight and carton structure so stiffness can be balanced with folding. |
| Coated vs. uncoated surface | The surface layer can crack differently from the fibres. | Approve the printed and finished sample on the selected stock. |
| Storage condition | Temperature and humidity history can change board response. | Ask how material will be stored and conditioned for the job. |
| Material change after approval | A substitute board can change fold appearance. | Require re-review if the board or supplier changes. |
Crease Rule and Matrix Selection
A crease is created by a matched system rather than one isolated number. The rule, counter material or matrix, channel geometry, board thickness, coating and job conditions work together to form a controlled hinge before folding. Technical guidance from paperboard and tooling suppliers consistently treats this as a board- and job-specific adjustment process.
A crease that is too weak may not guide the fold consistently. A crease that places excessive stress on the surface can make cracking more visible. The same setup should not be copied automatically between different boards, laminates, carton structures or production runs.
| Question | Why it matters |
|---|---|
| Was the rule and matrix reviewed for the actual board and finish? | Tooling needs to match the material and surface stack. |
| Are the critical folds standard, reverse, narrow or closely spaced? | Different fold geometry may require different review. |
| Was the crease tested after printing and finishing? | Coating or lamination can change the final response. |
| Does the sample use the intended die-cut and folding method? | A hand mockup may not represent production tooling. |
| Will a material or finish change trigger a new review? | Changing one layer can change the whole crease-and-fold system. |
Buyers should not copy rule or matrix dimensions from a generic online table into a purchase order. The packaging supplier should confirm the setup for the selected board and structure.
Ink Coverage, Coating and Lamination
Dark full-coverage printing can make exposed white fibres easier to see. Ink and coating layers can also show their own cracking patterns. Lamination adds another layer that can whiten, stretch or separate near a fold. These visible effects may overlap, which is why the symptom should be identified before the supplier changes the crease, board or artwork.
The artwork review should flag deep black panels, large solid colors, gradients, fine text and critical logos that cross a fold. If color consistency matters, coordinate the fold-risk review with the CMYK vs Pantone packaging color guide, but do not treat color-system selection as a cure for fibre cracking.
| Surface condition | Possible visible issue | Review step |
|---|---|---|
| Dark solid ink | White fibres or ink breaks become more visible. | Mark the critical fold and approve on the selected board. |
| Aqueous or UV coating | Fine surface lines or different gloss at the fold. | Review coating coverage and production-relevant sample. |
| Matte or gloss lamination | Whitening, stress marks or separation. | Review film, adhesive, crease, fold and storage together. |
| Multiple surface layers | More than one symptom may appear. | Inspect the fibre, ink, coating and film separately. |
Foil, Embossing and Spot UV Near Folds
Foil stamping, embossing, debossing and Spot UV can create premium carton details, but their position relative to a fold should be reviewed during artwork preparation. Tool pressure, raised or recessed areas, coating build-up and surface stiffness can change the way a fold looks and feels.
There is no universal clearance distance that fits every board and finish. Instead, mark the exact finish area on the dieline, identify the critical retail-facing fold and ask the supplier to confirm whether the layout should be adjusted before sampling.
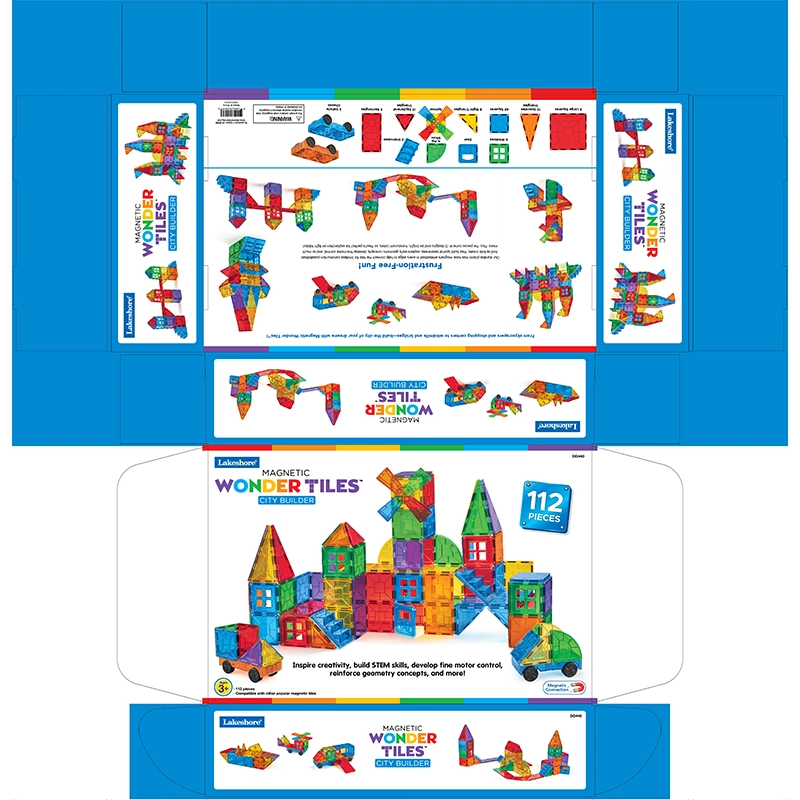
Use the print-ready artwork and dieline guide to organize cut lines, fold lines, bleed, safe areas and finish layers before technical review.
Folding Direction, Speed and Pre-Breaking
After creasing and die cutting, the blank still needs to be folded in the intended direction and sequence. Reverse folds, narrow flaps, high-speed machine folding and stiff laminated panels can behave differently from a slow hand fold. Pre-breaking or a first-fold review may be useful where the supplier offers it, but buyers should confirm the actual production method rather than assume every job includes the same step.
The sample should reproduce the relevant fold direction and final forming method whenever possible. If the buyer only receives a flat print proof or a hand-scored mockup, record that it does not approve production crease quality.
How Samples Reduce Score-Cracking Risk
Different sample types answer different questions. A digital sample can confirm artwork, layout and general color direction. A white dummy can help evaluate size and structure. A production-method sample is more relevant when the actual board, crease, lamination, foil, embossing or folding appearance is critical.
| Sample type | Useful for | Important limitation |
|---|---|---|
| Digital printed sample | Artwork, copy, layout and general color direction. | May not reproduce final board, ink, coating, lamination or crease tooling. |
| White structural dummy | Size, fit, opening, panel layout and basic folding sequence. | Does not approve printed or finished fold appearance. |
| Production-method sample | Actual or closer board, print, finish, crease and fold review. | Still represents a controlled sample, not every mass-production condition. |
| Mass-production first article | Final material, tooling and production setup review where available. | Requires an agreed hold-and-approval process before the run continues. |
The packaging sample guide explains the broader differences between digital, structural and production-method samples. Record what each sample is intended to approve.
Buyer Artwork and Specification Checklist
- Final dieline with cut, crease, perforation and glue areas clearly identified.
- Critical retail-facing folds marked on the artwork.
- Large dark solids, gradients and logos that cross a fold highlighted.
- Foil, embossing, debossing, Spot UV and varnish supplied as separate layers.
- Board direction, thickness or approved sample reference where available.
- Lamination or coating type and coverage.
- Product size, weight and how the carton will be opened and closed.
- Required sample type and what the sample must approve.
- Visual acceptance standard for exposed fibres, ink, coating and laminate appearance.
- Change-control rule if the board, finish, supplier or artwork changes.
For complete file-preparation requirements, use the print-ready artwork guide. For broader purchasing information, use the custom packaging quote checklist.
Production QC Checklist for Critical Folds
The buyer and supplier should agree on the inspection points before mass production. The checklist below is not a universal defect tolerance; it is a framework for defining the project standard. Use our printed box tolerance checklist to define the dimensional, registration, color, finish and fit criteria that apply to the approved carton project.
| Check | What to compare |
|---|---|
| Outer fold | Fibre exposure, ink break, coating line, laminate whitening and finish alignment. |
| Inner fold | Board delamination, fibre damage and structural opening. |
| Critical corners | Cracking at intersecting folds, locking tabs and narrow flaps. |
| Fold angle and panel alignment | Whether the carton forms squarely and closes correctly. |
| Special finishes | Foil, embossing, Spot UV or varnish near the fold. |
| Sample comparison | Whether production matches the approved visual reference and recorded changes. |
Use the custom packaging quality control checklist for the wider inspection plan covering print, structure, dimensions, finishing, packing and documentation.
What to Send for a Folding Carton Quote and Risk Review
- Carton dimensions, structure and intended opening direction.
- Product size, weight and packing method.
- Target board or approved reference sample.
- Full dieline and print-ready artwork.
- CMYK, Pantone, dark solid and metallic areas.
- Lamination, varnish, coating, foil, embossing, debossing and Spot UV.
- Critical folds and customer-facing surfaces.
- Required sample type and approval schedule.
- Existing defect photos or physical samples.
- Visual acceptance standard and inspection method.
- Quantity, delivery destination and packing requirements.
For product structures, material directions and current quote support, visit our custom folding cartons page.
Common Mistakes That Increase Score-Cracking Risk
- Treating all white fold lines as the same defect. Fibre, ink, coating and laminate symptoms require different review.
- Choosing board by GSM alone. Structure, coating, thickness and stiffness also matter.
- Applying a universal grain-direction rule. Grain should be reviewed against the actual carton and critical folds.
- Copying rule and matrix dimensions from another job. Tooling needs job-specific adjustment.
- Adding dark solids or foil across a fold after sampling. Artwork changes can change the visible risk.
- Using a digital proof to approve final crease quality. The production material and finish may be different.
- Changing board or lamination without re-review. The approved crease-and-fold system may no longer apply.
- Leaving acceptance standards undefined. Buyers and suppliers may judge the same fold differently.
- Expecting a zero-defect guarantee. The practical objective is controlled risk reduction and agreed inspection.
Technical References for Creasing and Folding
These sources support the general framework that paperboard, tooling, direction and finishing need job-specific review. Their product-specific settings should not be copied directly into another carton specification.
- Holmen: paperboard creasing and folding
- AIMS Group: creasing, folding and storage guidelines
- Marbach: counter plate and board/finish matching
- Peer-reviewed research on laminated paperboard creasing and folding
- Peer-reviewed research on coated paperboard foldability
This article provides packaging procurement and production-planning guidance. It does not replace board-supplier recommendations, tooling trials or a project-specific acceptance standard.
Folding Carton Score Cracking FAQ
Why do folding cartons crack on the score?
Score cracking can involve several different symptoms, including exposed fibres, ink cracking, coating cracking or laminate whitening. Possible contributing factors include board construction, grain direction, board condition, crease geometry, print and finish layers, folding direction and production conditions. A visual symptom alone does not prove one root cause, so the complete job should be reviewed.
Does paper grain direction always need to run the same way as the fold?
No universal grain-direction rule applies to every carton. Grain direction changes stiffness and folding behavior, but the preferred orientation depends on the board, structure, fold geometry, panel dimensions and converting method. Buyers should ask the packaging supplier to review grain direction as part of the job-specific material and dieline assessment.
Can lamination cause folding carton cracks?
Lamination can change surface stiffness and the way a fold appears, and it may show whitening, stress marks or separation near a crease. That does not mean lamination is always the root cause. The board, adhesive, film, crease setup, folding direction and sample result should be reviewed together.
Do dark colors make score cracking more visible?
Dark solid colors can make white fibres, ink breaks and coating cracks easier to see. Heavy coverage near a fold may also need closer artwork and production review. The buyer should mark critical dark areas on the dieline and approve them on the selected board and finish.
How close can foil, embossing or Spot UV be to a fold?
There is no single clearance distance that is correct for every project. The safe layout depends on the paperboard, finish, tooling, artwork scale, fold direction and required visual result. Flag these effects on the dieline and ask the supplier to review them before sampling.
Can a digital sample prove that a carton will not crack?
A digital sample can help approve artwork, layout and general color direction, but it may not reproduce the final board, crease, lamination, foil or folding method. A production-method sample is more useful for fold-risk review, although it still cannot guarantee that every mass-production piece will behave identically.
What should buyers approve before mass production?
Approve the board and finish direction, dieline, fold-sensitive artwork, production-method sample when required, visual defect standard and the inspection method for finished folded cartons. Also record any changes made after sample approval because they can change the risk profile.
What should I send for a folding carton score-cracking review?
Send the dieline, carton size, board description, print coverage, lamination or coating, foil, embossing, Spot UV, fold direction, product weight, sample expectations and photos of any existing defect. Include the required visual standard and identify the most critical retail-facing folds.
Request a Folding Carton Risk Review
Send the dieline, board direction, artwork, lamination or coating, special finishes, critical folds, sample requirement and existing defect photos. HS PACKFACTORY can review the brief and identify which material, artwork, sample and approval questions should be resolved before quotation.